 Contact Us
 (877) 248-1631
A shop-floor reverse lookup that ranks published spline sizes from a tooth count, major diameter, optional minor, and over-pins — then points you to custom carbide spline inserts. Most spline jobs do not stall because the insert cannot be ground. They stall because nobody can say, with a straight face,
Category: CNC Broach
Expanding Small Shop Capabilities with Single-Point CNC Broaching
Adding keyways and splines without adding dedicated broaching equipment For a small machine shop, adding new manufacturing capabilities often means investing in more equipment, finding additional floor space, or outsourcing work to a specialty shop. Single-point CNC broaching offers another option. With the proper tooling, setup, and programming, shops can
What Is the Difference Between a Blind Keyway and a Through Keyway?
Why relief features are critical when broaching blind keyways At first glance, a blind keyway and a through keyway may appear to differ only in how far the slot extends through the part. From a CNC broaching standpoint, however, the difference is much more significant. A through keyway allows the
Why Machine Shops Should Keep Spline Broaching In House
Reducing cost, protecting parts, and expanding machining capability Machine shops are built around one core capability: making parts. Yet when it comes to internal splines, many shops still send the work to outside broaching specialists. For some applications, outsourcing may be necessary. However, many internal and external splines can be
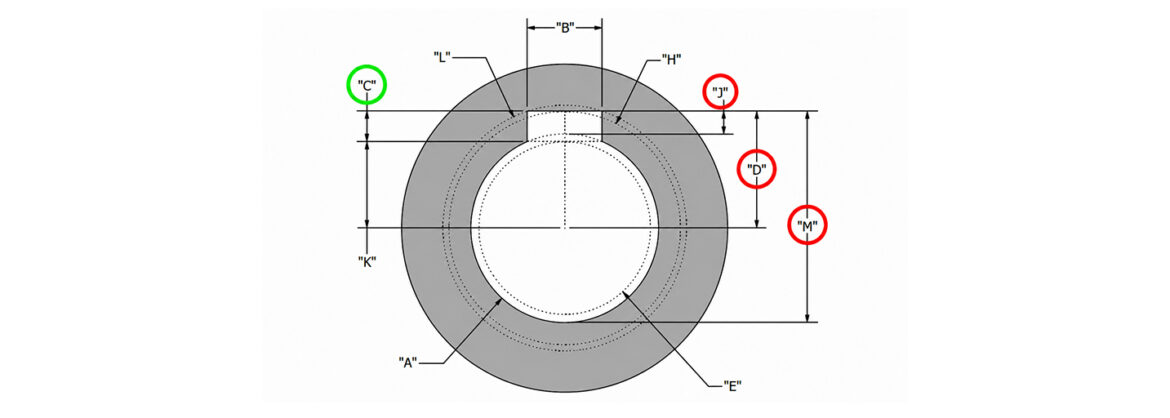
What Is the Height of Groove in Broaching?
Understanding the keyway dimension that is often overlooked When discussing a keyway, most machinists immediately focus on two dimensions: width and length. However, there is a third dimension that plays a major role in tooling selection and broaching feasibility. CNC Broach Tools refers to this radial depth as the Height
M19 Spindle Orientation Tips for CNC Broaching
When CNC broaching in a lathe or mill, the broach tool must stay aligned with the feature being cut. Since the spindle does not rotate during the broaching stroke, the cutting edge has to be oriented correctly before the tool enters the part. Many CNC broaching applications use an M19
Broaching Corners in Internal Hexes and Squares with CNC Broach Tools
Broaching internal hexes and squares can be handled with the same CNC Broach Tools holders and inserts already used for keyways, splines, and special profiles. Instead of broaching the entire shape in one pass, the process is usually done by machining the main walls first, then broaching each corner individually.
Why Does the Insert Need to Fully Clear the Cut Before Retracting?
Why exit clearance is critical for stable CNC broaching cycles Retracting the tool before the insert has fully cleared the cut can place side load on the cutting edge and shorten tool life. In CNC broaching, the insert is intended to cut under straight-line force, so exit clearance is an
How Do I Choose Between a Collet Holder and a Hydraulic Holder?
Choosing the right setup for rigidity, alignment, and consistent broaching performance Toolholding plays a major role in CNC broaching performance. Even with the correct insert and program, poor holder setup can lead to inconsistent cuts, insert wear, and unnecessary movement during the stroke. When choosing between a collet holder and
Why Domestic CNC Tooling Matters for Supply Chain Stability
Reducing risk and improving reliability in modern manufacturing Supply chain disruptions have become a regular concern for machine shops and manufacturers. Delays in raw materials, long lead times on tooling, and inconsistent availability can all impact production schedules. One area that is often overlooked is the source of CNC tooling.